Follow Us:

News

Who Decides Whether a Fridge Shelf Is Flat Enough? — KSHOW on Appliance Shelf and Bin Tooling

2026-11-18 0 Leave me a message

A shelf is a structural part dressed as a commodity

Walk through any appliance showroom and the shelves look like the cheapest thing in the cabinet. In tooling terms they are the opposite: a shelf is a long, thin, ribbed structural part with a visible cosmetic face, a food-contact surface and a fit interface that has to slide into a liner made on a different continent. Buyers who treat it as a commodity usually discover this at the first pilot run, when the shelf either rattles in its rails or will not enter them at all.

KSHOW has built injection mold tooling in Huangyan for 24 years, with 30,000+ molds delivered to 100+ countries under ISO 9001 and IATF 16949, and a fair share of that work is exactly this kind of unglamorous part: shelves, bins, crisper drawers, liners.

If you are re-sourcing a shelf or bin family, the useful first step is a liner drawing plus the load and temperature the shelf must survive: sale@taizhoumold.com, WhatsApp +86-18957424655. KSHOW will tell you which of the six tools in a typical family can share a mold base — and which cannot.

Clear polystyrene is unforgiving

The clear shelf is where a toolmaker's reputation is made or lost. General-purpose polystyrene transmits close to 90% of visible light, polishes to a mirror, and shows every flow mark, every weld line and every trace of residual stress as a bright band under supermarket lighting.

Three rules decide the outcome:

· Dry the resin and keep it dry. GPPS takes up only around 0.02% water as supplied, but a granule that has sat in a humid hopper can carry ten times that — and above roughly 0.1% the moisture turns to silver streaks on a clear face. Dry at 70–80 °C for 2–3 hours and keep the hopper dry.

· Gate where the flow can finish. A gate placed for mold convenience rather than flow balance lets the last melt arrive too late to pack, and leaves a hesitation mark that polishing cannot remove.

· Do not over-pack. Higher packing pressure improves flatness and worsens stress; a stressed clear shelf crazes in service when a customer wipes it with a solvent cleaner.MaterialLight transmissionMold shrinkageTypical roleMain riskGPPS88–90%0.4–0.6%Clear shelf, crisper frontCrazing under solvent attackHIPSOpaque0.4–0.7%White shelf, liner trimYellowing over timePPTranslucent to opaque1.2–1.8%Door bins, ribbed shelvesCreep under sustained loadPC88–90%0.5–0.7%High-temperature premium shelfCost and stress birefringenceKSHOW cuts clear-shelf cavities from ESR-grade mirror steel and finishes to a high polish, but the material choice in that table belongs to the appliance maker. The toolmaker's job is to make the chosen material behave — which is why the material grade has to be fixed before the cavity is polished, not after the first sample.

Where the tolerance actually lives

A shelf drawing usually carries one flatness callout and a general tolerance, and neither describes what the assembly line actually checks. The dimensions that stop a line are usually the ones the drawing never showed.

Short answer: rail spacing, front trim flatness, support pad height, bin hook geometry, molded scale marks and drawer run-out — six dimensions the assembly line checks, not the general tolerance on the drawing. Taken one by one:

· Rail spacing, typically 26 mm ±0.3 — 0.1 mm tighter and the shelf will not slide, 0.1 mm looser and it rattles.

· Front trim flatness, because it is the only line the customer sees when the door opens.

· Support pad height, which decides whether the shelf sits level or rocks on four points.

· Bin hook geometry, where a 0.2 mm error turns into a bin that drops when loaded.

· Molded scale marks and dividers, which must stay legible after the polish.

· Drawer run-out, since a crisper that binds at 80% extension reads as a quality defect, not a tolerance issue.

KSHOW agrees the datum scheme with the appliance maker before T0 for exactly this reason: if the shelf is measured against the rail centreline in the tool room and against the outer edge on the assembly line, both parties will be right and the part will still fail.

KSHOW case: six tools for one refrigerator platform

A Middle Eastern appliance brand was launching a 480-litre platform with four shelves and two door bins, and wanted one toolmaker for the whole set so that the parts would fit a liner that was already in production.

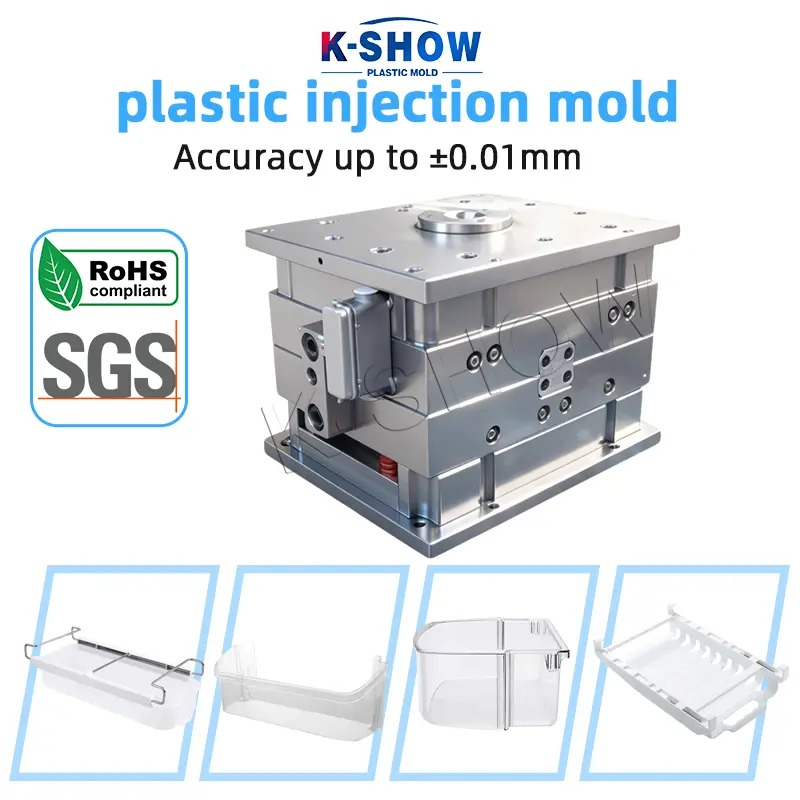
KSHOW cut six tools on three mold-base heights, so that one part family ran on two press sizes instead of six. The recorded project data:ToolPartMaterialCavitiesKey resultS1Clear shelf 480 × 320 mmGPPS1Flatness 0.45 mm vs 0.8 mm allowedS2Clear shelf 380 × 300 mmGPPS1Rail spacing 26.12 mm vs 26 ±0.3S3White shelf, ribbedPP1Deflection 2.1 mm at 15 kg, 24 h, 40 °CS4Half-depth shelfHIPS1Warp 0.6 mm, no rework after T1B1Standard door binPP2Hook pull-out 120 N vs 90 N minimumB2Deep door binPP21.2 m drop test, filled, no crackKSHOW has since repeated the same mold-base logic on other appliance families: fix the base by part family first, then schedule by press.

Two corrections were needed before release: a gate reposition on S1 to move a flow mark off the visible front third, and a 0.15 mm shim change on the S2 rail pocket. Scrap across the validation run fell from 6.1% to 1.4%, and the rail spacing on all six tools was still inside tolerance after 200,000 shots without re-shimming — the number the brand cared about, because a shelf that fits at launch and rattles at year three is a warranty claim, not a tooling issue.

What to send with the RFQ

Appliance shelf projects are decided by information, not by price per kilogram of steel. Five items shorten the path:

· The liner drawing with the rail profile, not just the shelf drawing.

· The load, temperature and duration the shelf must survive — 15 kg at 40 °C for 24 hours is a different part from 15 kg at 23 °C.

· The material grade and its food-contact documentation, fixed before polishing.

· Which surface is visible and which is hidden, so polishing effort goes where it is seen.

· The annual volume per variant, because a family of six low-volume tools is quoted differently from two high-volume ones.

KSHOW asks for all five before quoting a shelf family, and will say plainly when two variants should share a mold base and when sharing would cost more in changeover than it saves in steel. The question in the title has a short answer: the appliance maker decides what flat enough means, the molder decides whether it stays that way in service, and the toolmaker decides whether either of them can afford it. KSHOW works on the third answer first.

Short answers

Q: What tolerance actually decides whether a fridge shelf fits?

A: Rail spacing (typically 26 mm ±0.3), front trim flatness, support pad height, bin hook geometry — a 0.2 mm error drops a loaded bin — molded scale marks and drawer run-out. The general tolerance on the drawing decides none of them.

Q: Which material should a clear refrigerator shelf use?

A: GPPS for standard clear shelves: 88–90% light transmission, 0.4–0.6% shrinkage, main risk crazing under solvent attack. PC only for high-temperature premium shelves. The appliance maker fixes the grade before the cavity is polished.

Q: What should I send with an appliance shelf RFQ?

A: The liner drawing with the rail profile; the load, temperature and duration; the material grade with food-contact documentation; which surface is visible; and the annual volume per variant.

Q: What did the six-mold case achieve?

A: Flatness 0.45 mm against 0.8 mm allowed, rail spacing 26.12 mm within the 26 ±0.3 band, validation scrap down from 6.1% to 1.4%, and rail spacing still in tolerance after 200,000 shots without re-shimming.

Contact KSHOW

Have a part drawing? Let's price the mold.

Send the drawing, the annual volume and the target market. KSHOW checks manufacturability first, then quotes the tool — no obligation, no sales pitch.

Email sale@taizhoumold.com · WhatsApp +86-18957424655 · Web https://www.taizhoumold.comChannelDetailsCompanyTAIZHOU K-SHOW PLASTIC MOLD CO., LTDQualificationNational High-Tech EnterpriseAddressNo.18 Shangxian Road, Beicheng Industrial Zone, Huangyan District, Taizhou City, Zhejiang Province, ChinaPostcode318020ContactRichardPhone / WhatsApp+86-18957424655Emailsale@taizhoumold.comWebsitehttps://www.taizhoumold.comTrack record24 years

Published by: Jasmine

Reviewed by: Niki

Date: 18 November 2026

Related News
Leave me a message
X
We use cookies to offer you a better browsing experience, analyze site traffic and personalize content. By using this site, you agree to our use of cookies. Privacy Policy
RejectAccept