Thin-wall packaging—think yogurt cups, margarine tubs, deli containers, and thin-walled lids—represents one of the most demanding segments of the injection molding industry. Part wall thicknesses typically range from 0.25mm to 1.0mm, with flow length-to-thickness ratios often exceeding 200:1. Cycle times are measured in seconds (typically 3–8 seconds), and annual production volumes frequently exceed 10 million parts per mold.
As an experienced mold technician specializing in high-cavitation packaging molds, I have seen how small design flaws can become catastrophic in thin-wall molding. A gate imbalance of 5% can mean some cavities are over-packed while others are short. A cooling variance of 5°C can cause warpage that renders parts unusable at 1,000 parts per hour.
This article focuses on the key technical aspects of designing and manufacturing high-performance thin-wall packaging molds. Whether you are molding thin-wall containers, lids, or cups, understanding these principles will help you achieve faster cycles, better part quality, and longer mold life.
Thin-wall molding subjects molds to extreme conditions: very high injection pressures (up to 2,000 bar), rapid heating and cooling cycles, and high-velocity melt flow.
Recommended mold steels:
|
Steel Grade |
Hardness |
Key Properties |
Typical Application |
|
H13 / 1.2344 / SKD61 |
48–52 HRC |
High toughness, good thermal fatigue resistance |
Core and cavity plates, general thin-wall molds |
|
Stainless 1.2316 / S136 |
48–52 HRC |
Corrosion resistance for food-contact applications |
Packaging for acidic or wet products |
|
DC53 |
58–62 HRC |
Superior wear resistance for highly filled materials |
High-cavitation molds processing PP with >30% fillers |
Key consideration: For extremely high cavitation (e.g., 64 or 96 cavities), the mold base itself must be made from high-strength steel (e.g., P20 pre-hardened or 1.2738) to withstand injection pressure without plate deflection.
The hot runner is the heart of any thin-wall packaging mold. It must deliver melt to each cavity simultaneously with perfect balance, minimal pressure drop, and precise temperature control.
Critical design elements:
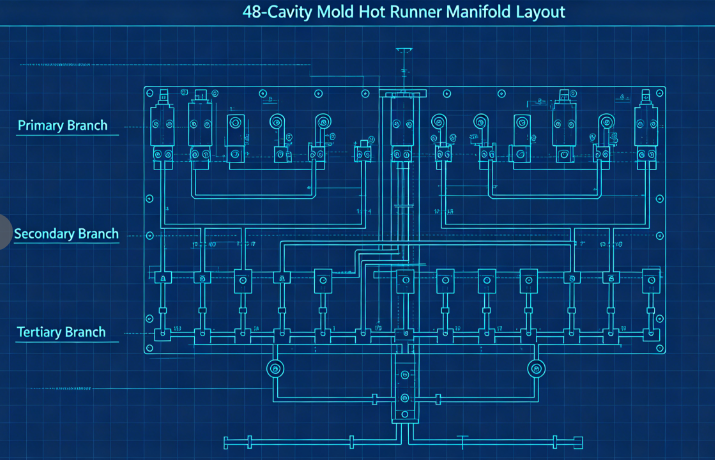
a) Balanced flow channels: For multi-cavity molds (typically 32, 48, 64, or 96 cavities), natural balancing is essential. This means each cavity has exactly the same flow length. A typical layout uses a primary manifold, secondary manifolds, and tertiary branches, all machined to identical dimensions.
b) Gate type and location: For thin-wall containers, the most common gate types are:Edge gates (for parts with a straight sidewall)Valve gates (for diaphragms or direct gating into the bottom)Submarine gates (for clean part-off without gate vestige)The gate must be sized correctly—too small, and shear heating causes degradation; too large, and gate vestige becomes unacceptable. Typical gate dimensions for thin-wall cups range from 0.8mm to 1.5mm in diameter.
c) Thermal balance: Each nozzle must have independent temperature control. Manifold channels should be heated uniformly (using dual-zone or three-zone heaters) to avoid hot spots or cold slugs.
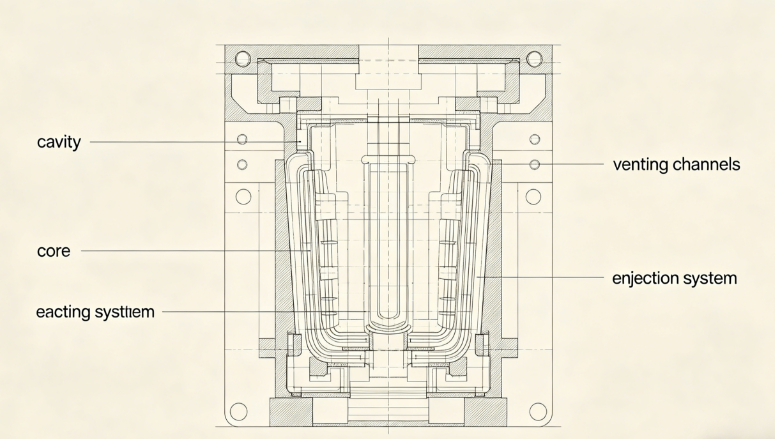
Thin-wall parts require extremely precise cavity and core dimensions to achieve consistent wall thickness.
Key considerations:
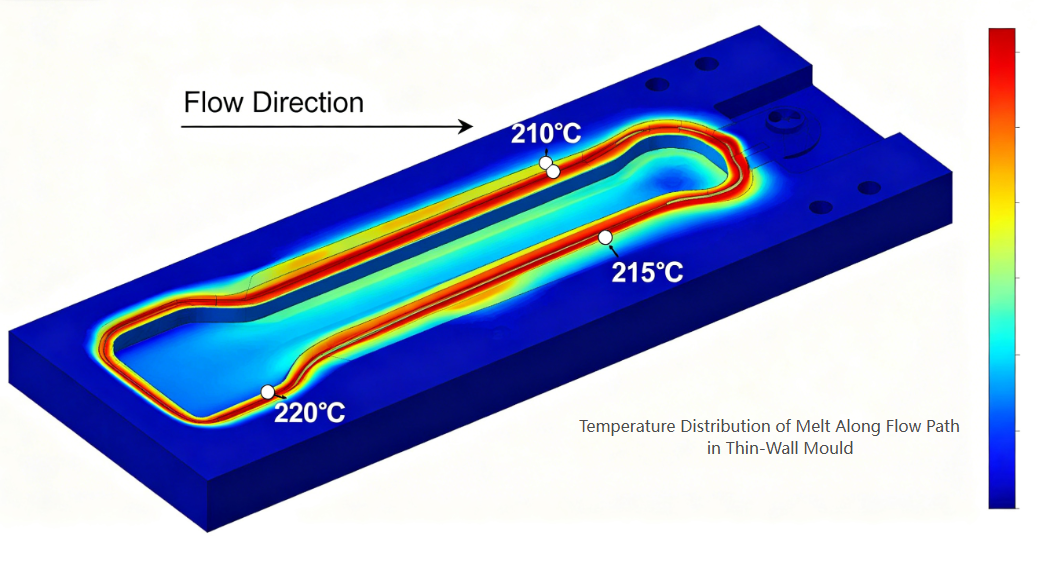
a) Wall thickness distribution: Maintain uniform wall thickness within ±0.02mm. Thickness variations create differential cooling and warpage. Use mold flow analysis to optimize the design before cutting steel.
b) Venting: Thin-wall molding uses high-speed injection (often 200–500 mm/s). Air trapped in the cavity must escape instantly. Recommended vent depths:0.02–0.03mm for PP0.01–0.02mm for PS or PET
Vents should be placed at the last point to fill, along the parting line, and around ejector pins.c) Draft angles: For thin-wall parts, minimum draft of 1° per side is recommended (1.5–2° for deeper containers). Insufficient draft leads to scratching, vacuum lock, and ejection problems.
d) Surface finish: Cavity surfaces for clear or glossy parts require SPI A-1 (mirror) finish; for opaque dairy containers, SPI B-1 (600 grit) is sufficient.
Cooling dominates the cycle time in thin-wall molding—typically accounting for 60–80% of the total cycle. Efficient cooling is the key to high productivity.
Design principles:
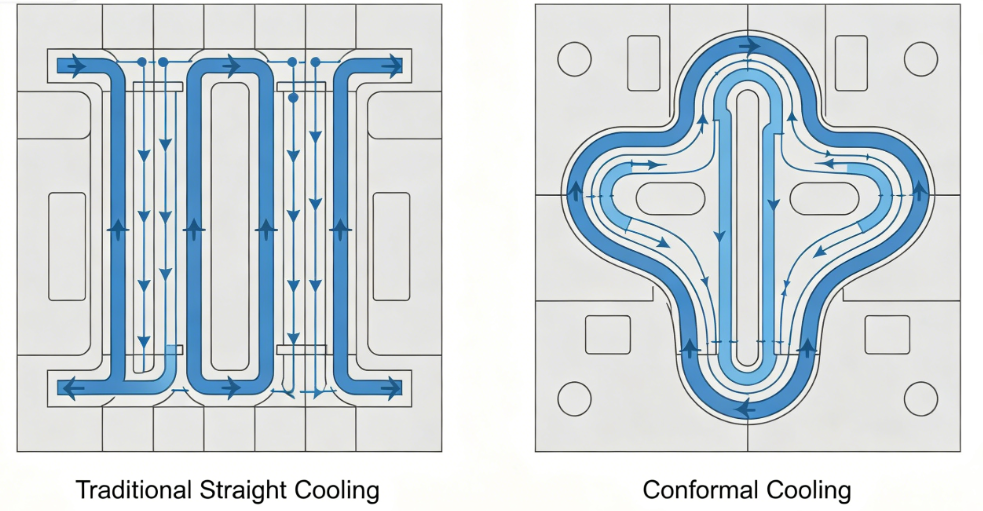
a) Conformal cooling: Traditional straight-drilled cooling channels are often too far from the cavity surface. Conformal cooling channels—following the contour of the part—can reduce cooling time by 30–50%. They are typically created using 3D printing or CNC machining of inserts with curved channels.
b) Cooling channel parameters:
c) High-efficiency cooling: Use bubblers or baffles in the core where space is limited. For tall cores, install spiral cooling inserts or heat pipes.
d) Cooling circuit separation: Independent circuits for cavity and core plates allow different flow rates and temperatures to optimize part release and minimize warpage.
Thin-wall parts are low in stiffness and can be easily deformed during ejection. The ejection system must be gentle yet reliable.
Design recommendations:
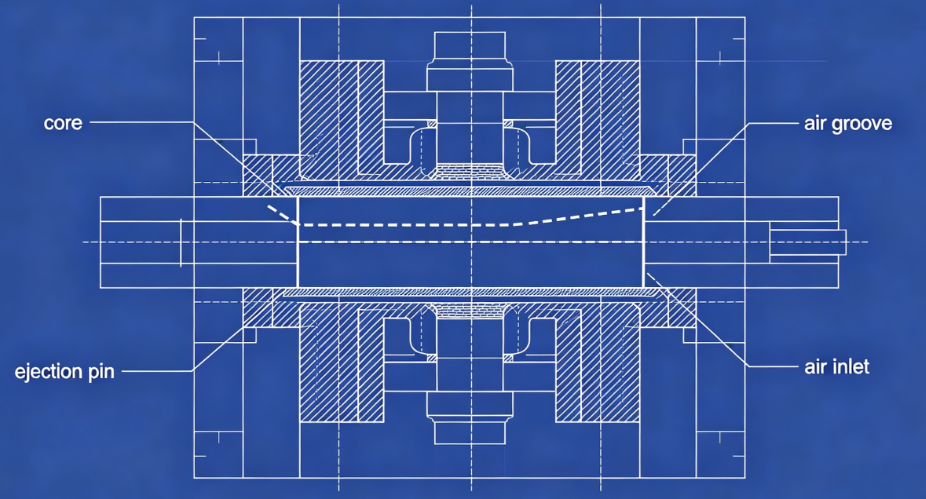
a) Air ejection: For many thin-wall containers (especially cups), air-assisted ejection is ideal. Compressed air (2–4 bar) is introduced between the core and the part through micro-grooves or porous inserts, floating the part off the core.
b) Stripper plate: For parts with undercuts or deep sidewalls, a mechanical stripper plate provides even ejection force across the entire part perimeter.
c) Ejector pins: When pins are unavoidable, use many small-diameter pins (2–3mm) placed on ribs or hidden surfaces. Avoid large pins that leave visible marks.
d) Timing: The ejection sequence should start only after the part has cooled sufficiently to avoid deformation. Use a short cool delay after mold open.
Even the best mold cannot produce good parts without proper process settings. Key parameters for thin-wall molding:
|
Parameter |
Typical Range |
Notes |
|
Injection speed |
200–500 mm/s |
High speed fills thin sections before freeze-off |
|
Injection pressure |
1,200–2,000 bar |
Required to overcome flow resistance |
|
Melt temperature |
190–240°C (PP), 230–280°C (PS) |
Optimize for viscosity |
|
Mold temperature |
10–25°C (cold runner) or 30–60°C (hot runner) |
Balanced cooling |
|
Back pressure |
5–15 bar |
For plastication consistency |
|
Defect |
Mold-Related Cause |
Solution |
|
Short shots |
Insufficient venting or undersized gates |
Add vents at flow endpoints; enlarge gates |
|
Warpage |
Uneven cooling or unbalanced filling |
Improve cooling uniformity; balance runners |
|
Sink marks |
Poor gate location or insufficient packing |
Relocate gate to thick section; add packing time |
|
Gate vestige too high |
Gate design improper |
Switch to valve gate or submarine gate |
|
Sticking on core |
Insufficient draft or air ejection failure |
Increase draft; clean air grooves |
|
Burn marks |
Inadequate venting |
Deepen vents within material limits |
Challenge: A customer required a 48-cavity mold for 150ml yogurt cups (PP, 0.45mm wall thickness, 4-second cycle, annual demand 20 million parts).
Actions taken:
Results:
Thin-wall packaging mold technology represents the pinnacle of injection mold engineering. The demands of high cavitation, sub-second cycles, and zero-defect production push every aspect of mold design to its limit. Successful thin-wall molds require:
Precision in cavity/core machining (±0.01mm)
Balance in hot runner flow channels
Efficiency in conformal cooling
Reliability in ejection systems
Understanding of material behavior and process dynamics
For mold makers willing to invest in advanced design tools and precision manufacturing, the thin-wall packaging sector offers tremendous opportunities—both in terms of technical challenge and business growth.
Phone: +86-18957424655
Mobile: +86-18957424655
E-mail: sale@taizhoumold.com
Address:No.18 Shangxian Road, Beicheng Industrial Zone, Huangyan District Taizhou City, Zhejiang Province, China
Copyright © 2025 Taizhou Huangyan K-Show Plastic Mold Co., Ltd. All rights reserved.